 跳到内容

A 37% failure rate on a pre-shipment inspection is the kind of number that stops a supply chain manager cold. That was the result of a 500-piece inflatable tent QC failure for a twelve-person glamping tent destined for a retail chain—a batch where the supplier’s own in-house QC had already signed off on visual appearance, missing every hidden weld defect that would have caused returns three months later.
The root cause wasn’t malicious or even unusual. One welding machine’s temperature drifted after a mid-run adjustment, and the production team kept running pieces because no one was checking air retention during the shift. The handmade sample the buyer approved had been welded on a different machine at lower speed, so it passed every aesthetic check. Mass production used a hotter, faster process that created invisible delamination around beam-to-floor connections and valve base separation at weld joints—defects no AQL 2.5 visual inspection will ever catch because most leaks are invisible until the tent is inflated and left untouched for hours.
This is why pressure-hold testing needs to be a separate contract line item, not an afterthought buried in the QC checklist. A standard pre-shipment inspection inflatable tents protocol without an air retention test is functionally useless for this product category. The benchmark you should write down for your next supplier call: any factory producing inflatable structures should be able to demonstrate a maximum pressure drop of less than 10% over twelve hours on every unit before packing.
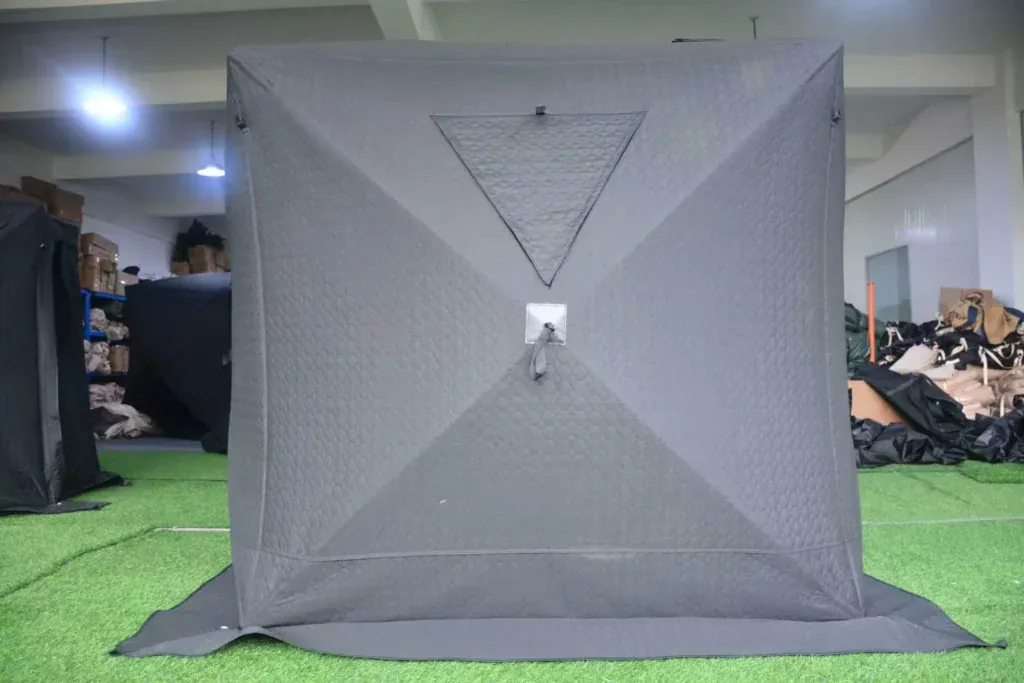
What Pre-Shipment Inspection Found
A standard AQL 2.5 visual check misses every air leak that matters.
The buyer’s third-party inspector arrived at the factory on day 38 of a 45-day lead time. The supplier had already issued its own QC report showing a 98% pass rate on visual checks. Stitching was straight. Zippers ran smooth. Logo placement looked correct. The inspector pulled 80 units from the 500-piece batch for a standard AQL Level II random sample.
37% failed the pressure drop test
The inspector inflated each sample tent to the specified working pressure, sealed all valves, and let them sit for 12 hours. By hour six, 30 of the 80 tents had lost more than 15% of internal pressure. That is not a slow leak from a pinhole. That is a structural failure in the air retention system. A standard AQL 2.5 inspection would have passed these units because the leaks are invisible until the tent holds pressure over time.
溶接部に生じたバルブ底部の分離
詳細な調査の結果、問題はTPUコーティング生地と溶接フランジが接するバルブ底部に集中していることが判明しました。12ケースでは、溶接ビードが基材から0.5mm未満剥離しており、これだけで一晩中空気が漏出する原因となりましたが、テープメータでステッチラインを追う視覚検査では見逃されるような微細な状態でした。根本原因は、稼働途中の調整後に温度が漂移(ドリフト)した単一の溶接工程へと遡りました。
ビームと床パネルの接続部周辺の層間剥離
8テントで、メインエアビームがフロアパネルに取り付けられるビーム・ツー・フロア溶接シームに沿って層間剥離が見られました。この部分は使用時の加圧・減圧サイクルで繰り返しストレスがかかります。剥がれのパターンは、RF溶接時の熱圧力にばらつきがあったことを示唆しており、おそらく3週間前に承認されたハンドメイドサンプルと異なる溶接プロセスで生産されたことが原因でした。
ロゴの位置と色の不一致
Where the Process Broke Down
サンプルは完璧に見えました。
買い手は見た目だけで試作サンプルを承認しました。縫い目は真っ直ぐで、ファスナーも滑らかに動き、生地色も潘トン指定色コードと一致していました。エア漏れが生じないか確認するため、空気を入れて12時間放置する検査は誰も行いませんでした。
溶接工程におけるインライン検査の実施なし
工場は2シフトで3台のHF溶接機を稼働させていました。生産4日目の朝、ライン作業者による稼働中の調整後、#2機の温度コントローラーが設定値より8℃高く drift しました。そのシフトで生産された87テントのうち、ビーム・ツー・フロア接合部に部分剥離が見られました。 ビームと床パネルの接続部. そのラインに配属されていたインライン検査担当者は、ファブリックパネルのステッチ品質を確認しており、溶接の健全性は点検していませんでした。
圧力テストがQCチェックリストから除外されていた
供給業者のQCチェックリストには23の検査項目(ファスナー動作、糸張力、ロゴ位置合わせ、生地色、継ぎ代など)がありましたが、気密性(空気保持)に関する項目はゼロでした。これは、インフレータブルテントを「チューブポケットを追加しただけの従来のテント」と扱いがちな工場に一般的に見られる問題です。標準的なAQL 2.5の視覚検査では、テントに空気を込めて数時間放置しなければ現れない大部分のリーク欠陥は見逃されます。
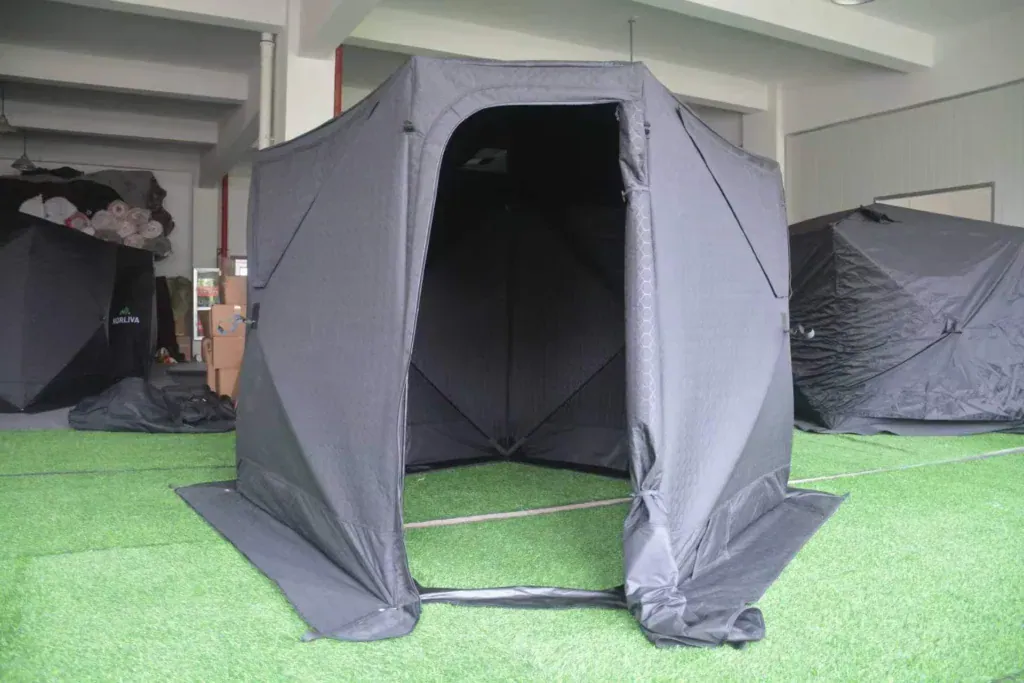
是正処置の判断が品質管理ではなく生産側によって行われた
出荷前検査員が圧力低下不良を指摘した際、工場側の生産マネージャーは、品質管理チームへの相談や買い手への事前報告 없이、失敗した全ユニットに対して貼り付け・再加圧という応急修理を承認しました。この修理は1時間は持ちましたが、37テント中14テントで翌朝には再び失敗しました。その時点ではコンテナ積付けのタイムスケジュールは既に確定していたため、対応を余儀なくされました。
How a Structured QC Checklist Would Have Caught It
A standard AQL 2.5 visual inspection misses air retention defects entirely.
The first fix is a pre-production meeting where the buyer and factory agree on pressure drop limits in writing. For a twelve-person glamping tent with a target operating pressure of 8 psi, the acceptable loss over 12 hours should be defined before the first meter of fabric is cut. Without this number, there is no pass/fail criteria.
First Article Inspection After the First 50 Pieces
After the first 50 units come off the line, stop production and test them. This catches drift early. In this case, one welding machine’s temperature drifted after a mid-run adjustment — that would have been visible in the first article batch if anyone had inflated those tents and measured pressure loss.
Random Sampling at 25%, 50%, and 75% of Production
Three sampling gates during production build a trend line. If failure rates climb at the 50% mark, you can halt rework before another 250 units are welded. The supplier’s QC team needs to run an air retention test on a fixed sample size at each gate, not just a visual check of seam appearance.
Final Pre-Shipment Inspection With Clear Pass/Fail Criteria
The final inspection must include an air retention test as a separate contract line item — not buried inside an AQL visual checklist. The standard used by Kelyland Outdoors’ partner factories, which operate under ISO 9001:2015 protocols, includes inline welding checks and documented pressure testing before packing. That level of process control turns a subjective review into a measurable pass or fail.
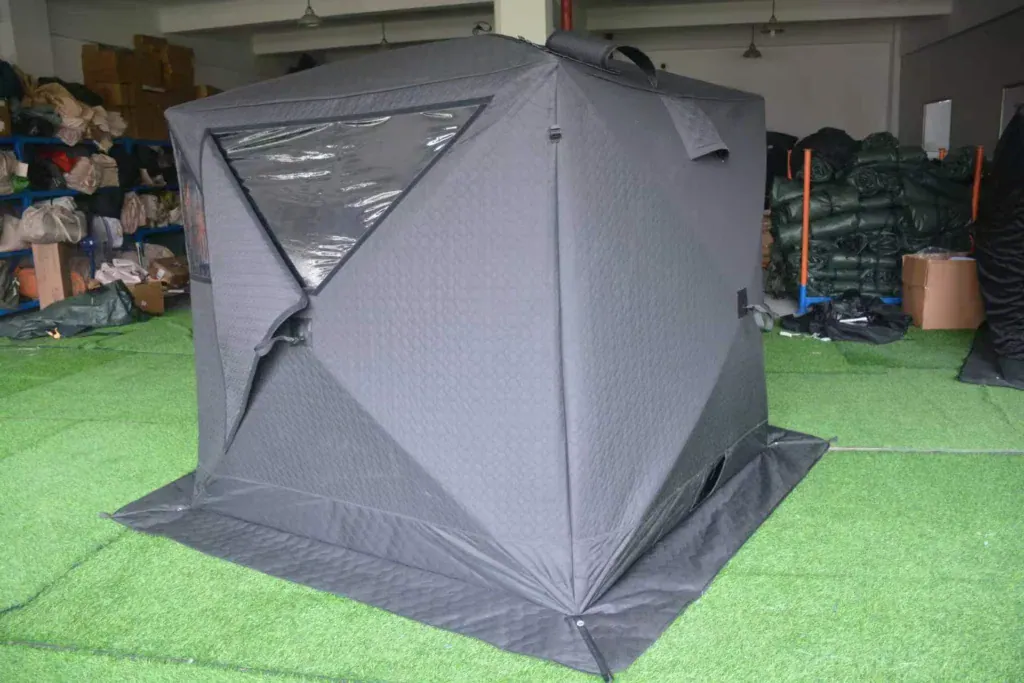
What the Buyer Did Next
The buyer turned a $50K near-miss into a permanent process upgrade.
The supply chain manager didn’t cancel the order. That would have meant losing the season entirely, with a retail launch already locked in for April. Instead, he negotiated rework terms directly with the factory owner. Every tent that failed the pressure test — 185 units out of 500 — was pulled from the shipping batch and sent back to the welding station. The factory covered all material costs and labor for re-welding every valve base and beam-to-floor joint. The buyer agreed to split the expedited shipping fee to keep the delivery window intact.
Negotiated Rework, Not Full Rejection
Full rejection would have triggered a six-month production delay at a different supplier. Rework cost the factory roughly $12 per unit in additional labor and materials, versus an estimated $85 per unit in lost margin if the order was scrapped. The math worked for both sides. But the buyer made one thing clear: this was a one-time concession. Future orders would require documented proof of air retention testing before any shipment left the factory floor.
Implemented a Mandatory Air Retention Test on All Future Orders
The old contract specified visual inspection only — standard AQL 2.5 sampling on stitching, zippers, and fabric defects. That caught nothing on air retention because most leaks are invisible until the tent holds pressure for hours. The new contract added a separate line item: 100% inflation testing on every unit, with a maximum allowable pressure drop of 10% over 12 hours at room temperature. Any unit exceeding that threshold gets flagged for weld inspection before packing.
Added a Line-Item for Weld Inspections in the Production Contract
The revised contract now specifies inline weld checks at three points: after the first 50 units (first article inspection), at 50% of production volume, and again during pre-shipment inspection. Each check includes both visual examination of weld bead consistency and a short-duration pressure hold test on randomly selected units from that batch. This mirrors how partner factories in Kelyland Outdoors’ network handle inflatable tent production — with inline welding checks and documented pass/fail criteria before bulk assembly continues.
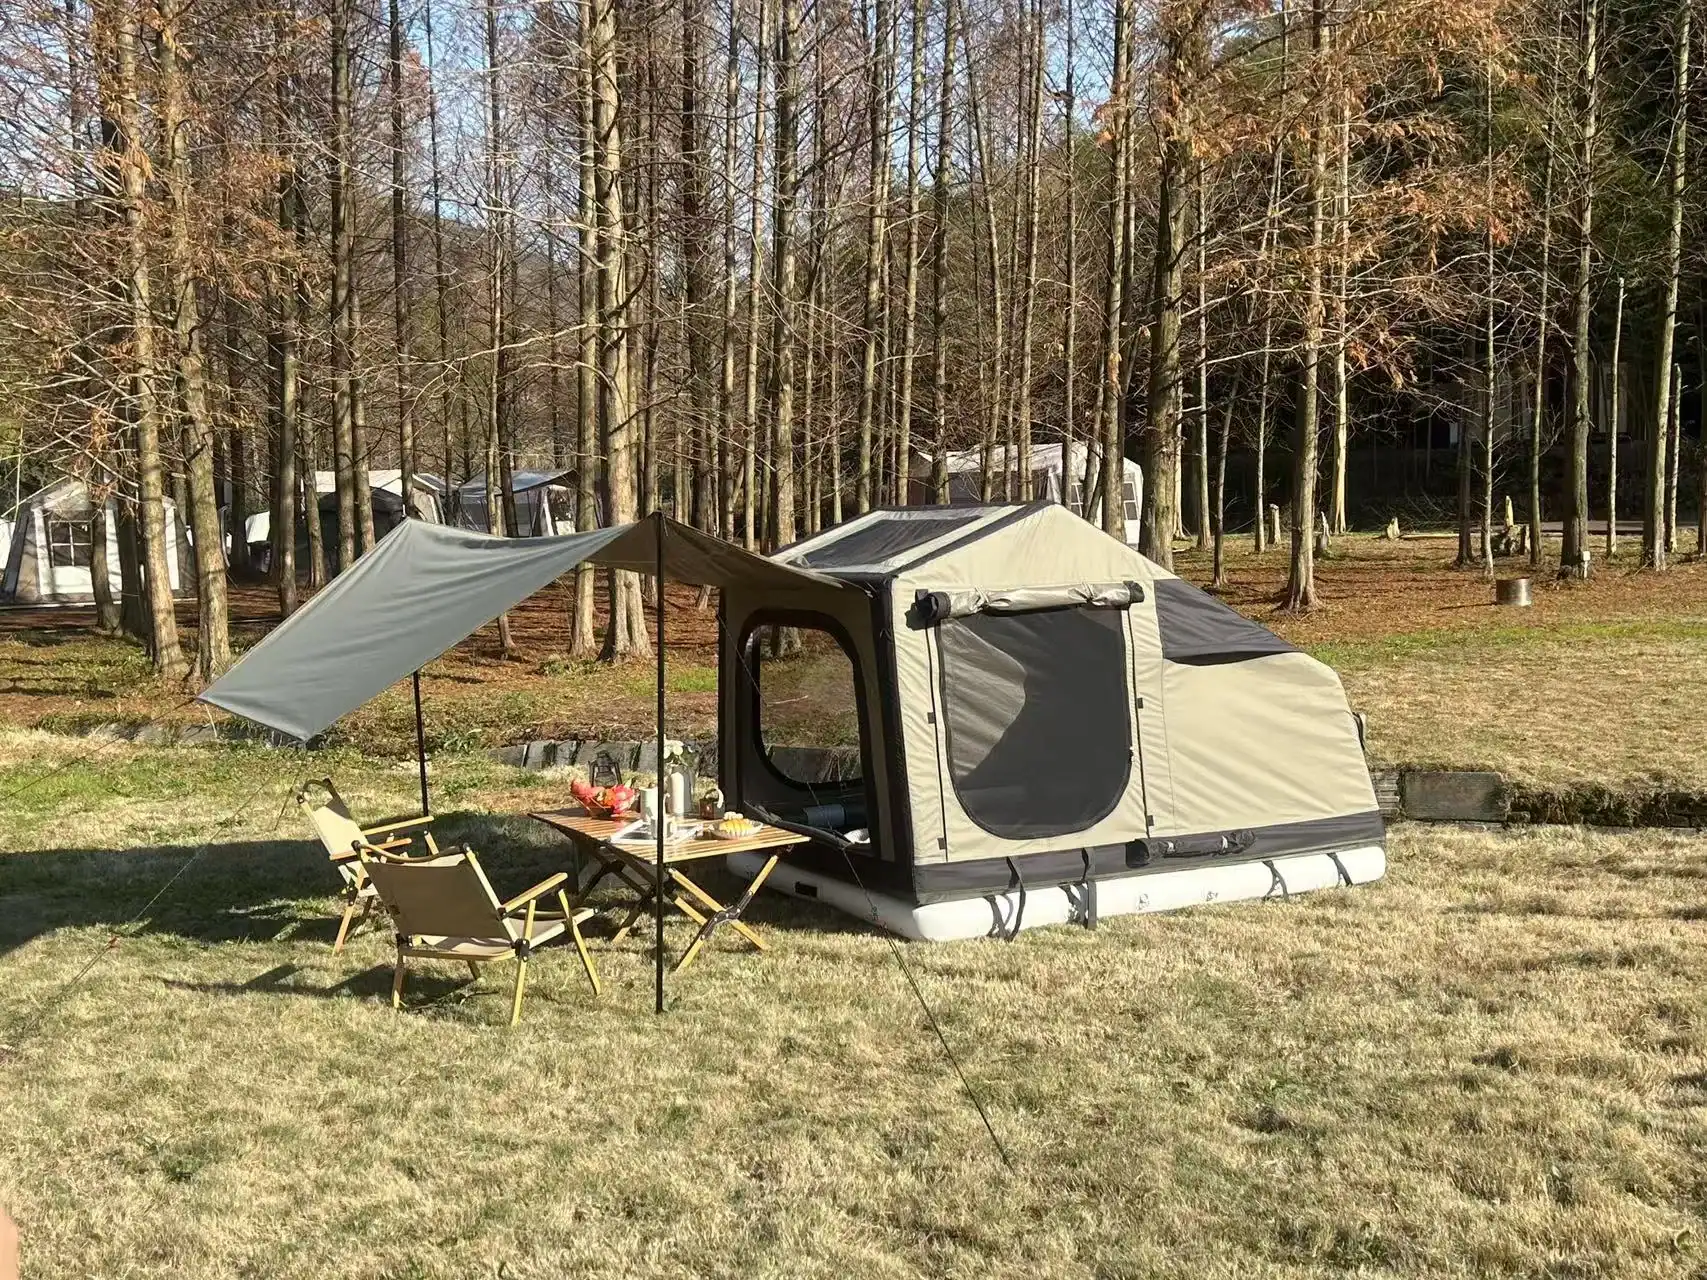
How Kelyland Outdoors Prevents These Failures
Three QC steps that directly address the welding drift and invisible leak failures from the 500-piece case study.
The 500-piece order failure traced back to a single root cause: a welding machine whose temperature drifted after a mid-run adjustment. The factory’s QC team was checking visual appearance only, so no one caught it until the buyer’s pre-shipment inspection flagged 37% of units for pressure loss. That scenario repeats across inflatable tent sourcing because most suppliers treat air retention as a design assumption, not a production variable.
100% Inflation Testing Before Packing
A standard AQL 2.5 visual inspection will not catch air retention defects. Most leaks are invisible until the tent is inflated and left untouched for hours. At Kelyland Outdoors, every inflatable tent unit — whether from the Xiangyang air mattress factory (2.5 million units annual capacity) or the Ningbo tent factory — undergoes a full inflation hold test before packing. Each unit is inflated to rated pressure, sealed, and monitored for at least 30 minutes. Units that lose more than 5% pressure are flagged for weld inspection and rework.
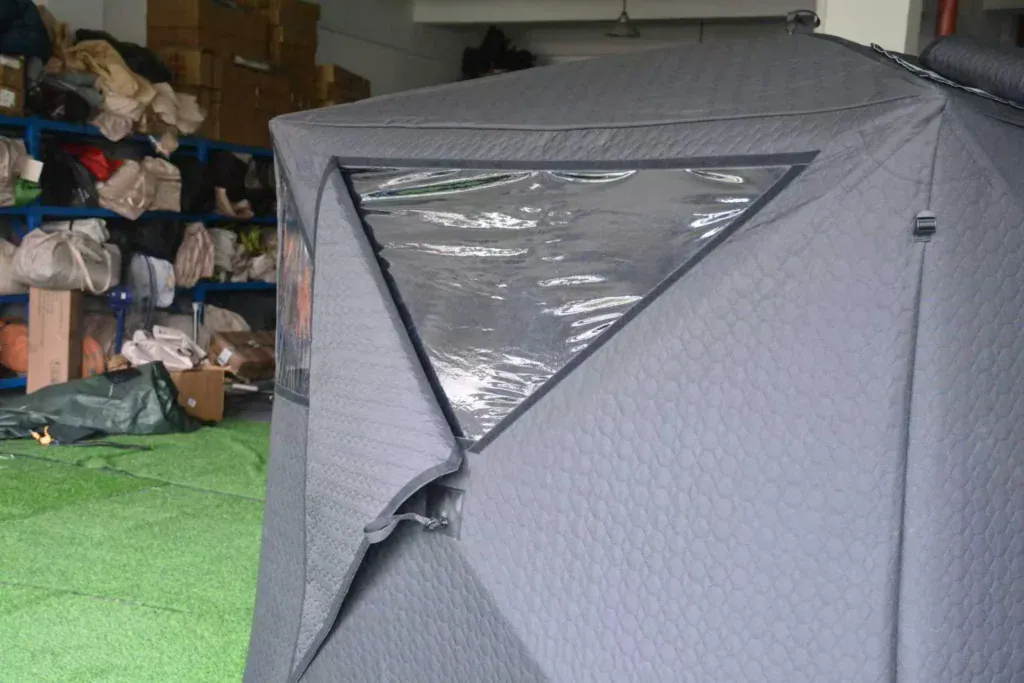
Inline Welding Checks at Strategic Factories
The case study’s welding drift happened because inspectors only checked finished tents. By then, all 500 units had passed through the same drifting machine. The fix is inline checks during production, not after. Kelyland’s partner factories — including ISO 9001:2015 certified facilities in Zhejiang and Hubei — run weld temperature verification every 50 joints during mass production runs. If a machine drifts by more than ±5°C from the approved spec, production stops until recalibration is confirmed.
Clear QC Deliverables for Every Order
The supplier in the case study had no written pressure drop limit in their QC checklist. The buyer hadn’t specified one either. That gap is common when sample approval focuses on aesthetics alone — handmade samples look great but hide process inconsistencies from mass production tooling. Kelyland Outdoors includes three mandatory QC deliverables in every inflatable tent contract: a signed first article inspection report after the first 50 pieces, an inline weld temperature log from each production shift, and a final air retention test result with pass/fail thresholds agreed during pre-production.
結論
That $50K order was salvaged through rework, but the timeline blew past the retail launch window. A standard AQL 2.5 visual inspection missed every air retention defect because those leaks only show up after hours of inflation. The fix isn’t a better inspector — it’s a contract line item for a 12-hour pressure-hold test.
-
- 37% of units failed a 12-hour pressure drop test in this case.
- Visual-only sample approval misses weld defects from mass production.
- Pressure-hold testing must be a separate contract line item.
- Inline welding checks catch temperature drift before it affects the batch.
Before you approve your next inflatable tent production run, ask your supplier three yes/no questions from the checklist above — starting with whether their QC protocol includes an air retention test on every unit, not just a visual pass. If they hesitate on the pressure-hold spec, you already know where this story heads. Review how Kelyland Outdoors builds that test into every order by browsing our inflatable tent and air mattress production standards.
よくある質問
How to get a quote for Inflatable Tent QC Failure: 500-Piece Order Case Study?
正確な回答は、製品仕様、数量、および注文条件によって異なります。最も安全な方法は、最終要件シートが確定した後にのみ商業条件を確認することです。.
最初にサンプルを依頼できますか?
正確な回答は、製品仕様、数量、注文設定によって異なります。最も安全な方法は、最終的な要件シートが確定した後にのみ、商取引条件を確認することです。.

 English
 Español
 Deutsch
 Français
 Português do Brasil
 Русский
 العربية
 한국어
 日本語