 콘텐츠로 건너뛰기

inflatable tent fabric denier is the first checkpoint buyers should lock before they approve a supplier, budget, or production slot. A buyer’s checklist for an inflatable tent order looks solid on paper: approved sample, confirmed FOB pricing, signed spec sheet. Then the mass production run lands, and the shell fabric feels thinner than the swatch you held. The coating on the air beams starts showing a white residue after three days in storage. That $50K order turns into a season of returns because nobody flagged the one item that causes most post-delivery complaints — whether the inflatable tent fabric denier and coating actually match between sample approval and bulk production.
The gap between a pre-production sample and a full container load is rarely about the big specs. It’s about consistency in weave density, coating adhesion, and tear propagation resistance across rolls from different production lots. A 210D ripstop with proper tear strength will outperform a 300D plain weave that lets a small cut run across an entire panel. And on the beam fabric side, PVC-coated material can look identical to TPU until you fold it tight and check for plasticizer migration — that sticky or powdery residue signals early failure.
A solid benchmark here is asking for an ISO 13937 tear test report and comparing it against your own swatch fold test during factory visits. If the supplier’s lab report shows tear strength below 30 Newtons for a shell fabric rated at 210D or higher, you have a problem waiting to happen in windy conditions.
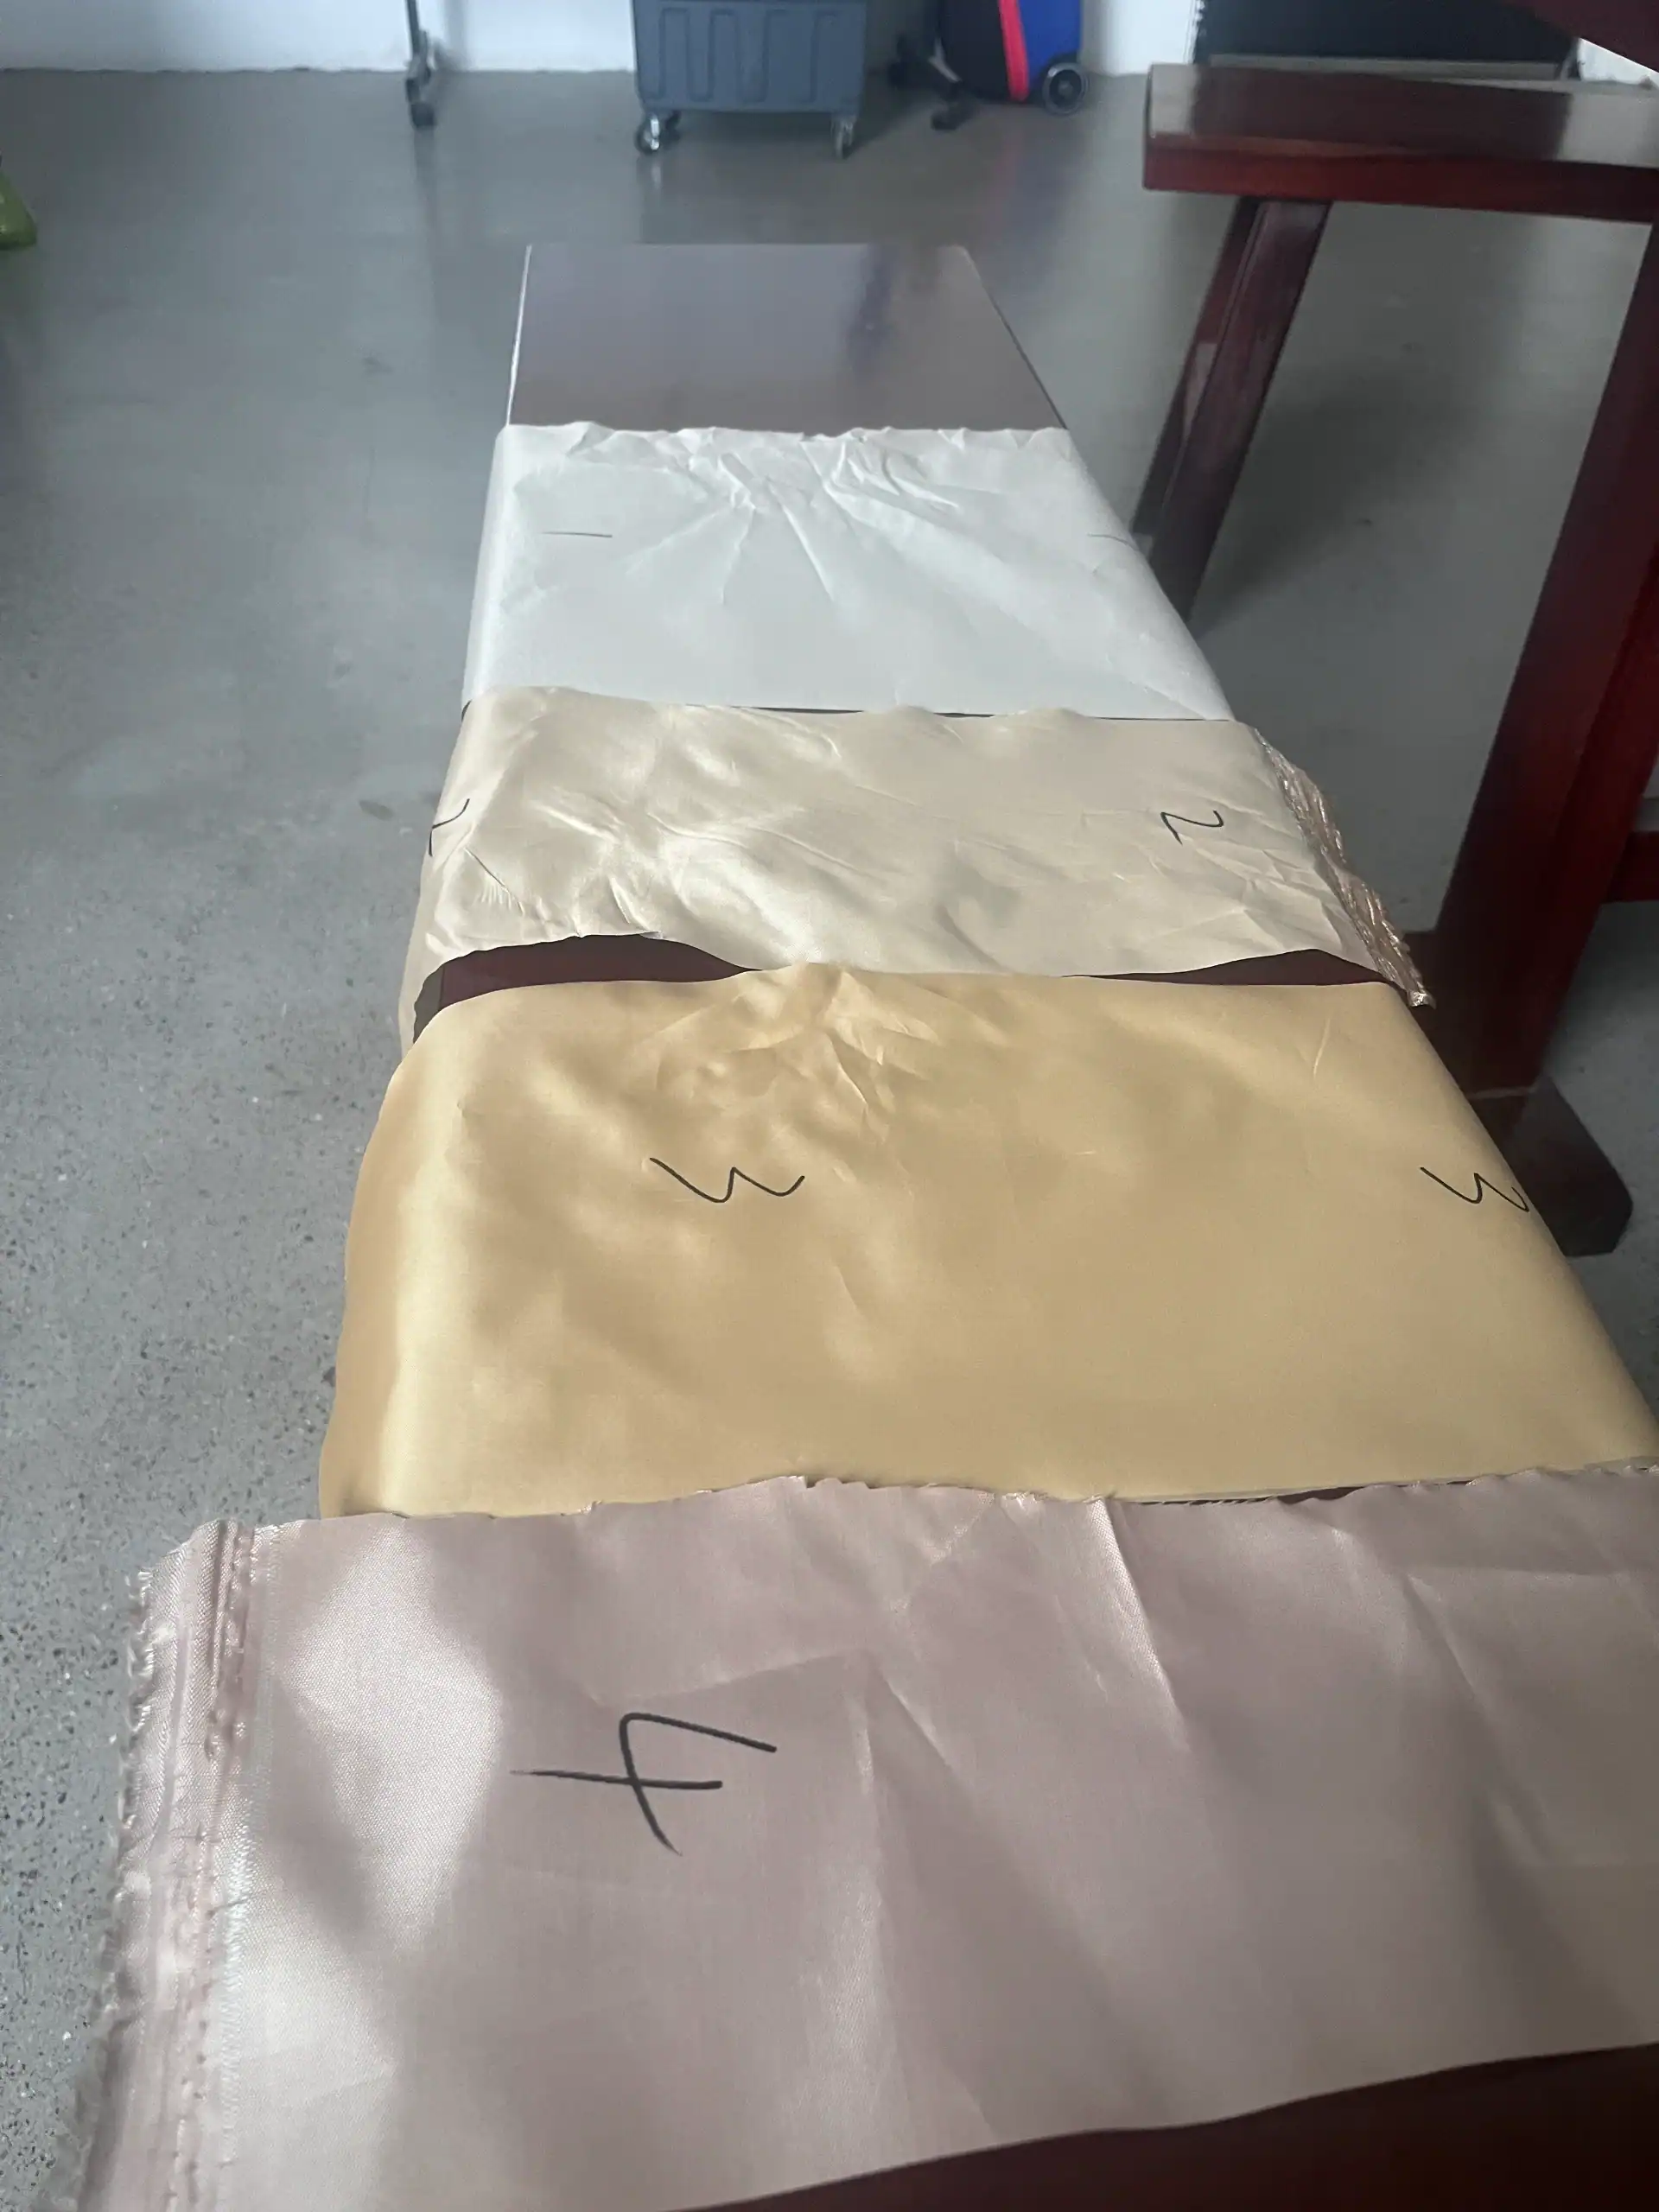
Why Fabric Turns a Great Inflatable Tent Design Into a Failure
The shell fabric and the air beam fabric fail in completely different ways.
Most buyers focus on the outer shell fabric because that is what they see and touch during sample approval. They run a hand over a 300D polyester oxford, feel the thickness, and approve the order. Meanwhile, the real failure point is already sitting inside the beam tubes — a PVC coating that will start plasticizer migration after three months of warehouse storage in summer heat.
How shell fabric rips in wind and UV sunlight
Shell fabric failure usually starts with UV degradation, not an immediate tear. A standard polyester oxford without UV-resistant coating loses about 40 percent of its tensile strength after 500 hours of direct sunlight exposure. That weakened fabric then encounters a gust at a campsite — and a small abrasion point becomes a running tear across the entire panel. The weave structure matters more than denier here. A 210D ripstop weave with reinforcing threads every 5mm will stop a tear from propagating. A 300D plain weave without ripstop grid lets that same cut run end to end.
How beam fabric delaminates and softens over seasons
The air beam fabric faces a completely different stress profile. It is under constant internal pressure, flexed at every fold point during setup and takedown, and exposed to temperature swings from -10°C to 50°C inside the tube. The most common failure mode on PVC-coated beams is delamination between the base textile and the coating layer. When plasticizer migration occurs — you can detect this by folding a sample tightly for 24 hours and checking for white powder or sticky residue — the coating loses flexibility. Cracks form along fold lines, and the beam develops slow leaks that are nearly impossible to field-repair.
Key Fabric Specifications to Put in Your Custom Build
Shell fabric and air beam fabric need different specs.
Most buyers focus on denier when specifying inflatable tent fabric. They assume a higher number means stronger material. That logic holds for shell fabrics but breaks down completely when you look at the air beams underneath. A 300D oxford shell can feel tough while the TPU or PVC-coated beam fabric fails after two seasons because the coating delaminated, not because the base textile ripped.
Denier and weave: 150D vs 210D vs 300D polyester oxford
Denier measures the linear mass of individual fibers. A 150D yarn is thinner than a 300D yarn, but weave construction matters just as much. A 210D ripstop weave with reinforcing threads every few millimeters can outperform a 300D plain weave in tear propagation resistance. The key metric is how far a small cut travels before hitting a reinforcement grid.
For inflatable tent shells, the practical floor sits at 210D for lightweight backpacking models and climbs to 300D or higher for family glamping tents that see rougher handling and more UV exposure. Anything below 150D risks punctures from branch contact or abrasion during setup.
PVC vs TPU coated fabric for air beams
The air beam is where most cost-driven failures happen. PVC-coated fabric dominates the budget segment because raw material costs are lower and lamination is simpler. The trade-off comes after two or three years of use: plasticizers in PVC migrate to the surface, making the coating brittle and prone to cracking at fold points.
Black coating provides superior UV protection to prevent fabric degradation over seasons
Simple Swatch Tests for the Showroom or Factory Visit
A sharp fold at 90 degrees reveals coating brittleness in seconds.
You don’t need a tensile tester to catch bad fabric. Three manual tests, done in the showroom or on the factory floor, will flag the most common failure modes before you commit to a production run. These take about five minutes total and require nothing but your hands and eyes.
Fold Test for Coating Cracking
Take a palm-sized swatch of the coated fabric — shell or beam material, it doesn’t matter. Fold it sharply at 90 degrees along the same axis, press the crease hard with your thumbnail, and unfold. Look at the crease line under direct light. If you see white stress marks, micro-cracks, or any powdery residue flaking off, that coating will fail within two seasons of regular setup and takedown. On PVC-coated fabrics used for air beams, this test is non-negotiable because beam flex during inflation cycles concentrates stress on the same fold lines repeatedly.
Tear Propagation Test with a Small Notch
Cut a 5mm slit at the edge of a fabric sample — use scissors or a knife. Hold the fabric on both sides of the notch and pull steadily in opposite directions. A quality ripstop weave will stop the tear at the first reinforcing thread. A plain weave with low tear strength will let that small cut run straight across the panel without resistance. This is where a 210D ripstop polyester outperforms a 300D plain weave every time: higher denier means nothing if a single snag turns into a structural failure.
Weight, Hand Feel, and Color Consistency
Hold two samples from different parts of the same roll side by side. They should feel identical in weight per square meter — any noticeable difference suggests uneven coating application or inconsistent yarn tension during weaving. Rub the surface between your fingers; cheap coatings often feel tacky or waxy while quality PU or silicone finishes feel smooth and dry. Check color under natural daylight, not fluorescent shop lights. A batch mismatch of even half a Pantone step becomes obvious when panels sit next to each other on an assembled tent.
Third-Party Test Reports to Request from the Supplier
A single lab report can save you from approving a fabric that fails in month 6.
Most suppliers will tell you their fabric is waterproof. The question is: how waterproof, and for how long? The ISO 811 hydrostatic head test is the industry standard for measuring water penetration resistance. A fabric sample is clamped under a column of water, and pressure increases until three droplets break through. For inflatable tent shells, a minimum of 3000mm hydrostatic head rating is expected. For floor fabrics or rainfly panels, 5000mm or higher is common. If the supplier cannot produce an ISO 811 report from an accredited lab, you are accepting the claim on trust alone.
ISO 13937 tear strength test
Denier tells you thread thickness. Tear strength tells you whether the fabric holds when a sharp rock or branch contacts it. ISO 13937 measures the force required to propagate a tear across a fabric panel after a small initial cut has been made. This matters more than raw denier because a tightly woven plain-weave fabric can fail catastrophically when nicked, while a ripstop weave with reinforcing yarns at intervals will stop the tear from spreading. Look for reports showing tear strength above 15N for shell fabrics and above 25N for beam fabrics.
UV resistance and flammability test reports
UV degradation is invisible until the coating starts flaking and the base fabric loses tensile strength. Request a UV resistance report based on ISO 4892 or AATCC TM16 standards — typically after 500 hours of accelerated exposure. The acceptable threshold depends on your target market: European retailers often require no more than 20% strength loss after testing. Flammability certification varies by region but CPAI-84 (for tents) and BS EN ISO 6941 are common benchmarks in North America and Europe respectively.
켈리랜드 아웃도어 partners with factories that maintain CE and ISO 9001 certifications across multiple product lines — including dedicated tent facilities in Ningbo producing up to 800,000 units annually with documented quality control at every stage of production.
Red Flags That Signal Cheap Fabric
Three red flags that cost one buyer $50,000 when his pre-production sample passed but the mass production run didn’t.
A cheap PVC coating often smells like a chemical spill. That sharp, sweetish odor isn’t just unpleasant — it signals excessive plasticizer content. Plasticizers make PVC flexible, but too much means the coating will leach out over time. The result? A sticky residue on the fabric surface after a few months in storage, and a beam that stiffens and cracks as it loses flexibility. If you catch that smell during a factory visit, flag it immediately.
Whitening of the coating when bent
Take a corner of the fabric sample and fold it sharply. If the crease turns white or shows a powdery line, the coating has fractured. That white mark is delamination — the bond between the coating layer and the base fabric has broken at a microscopic level. In an inflatable tent beam, that crease zone becomes a stress concentration point. Under repeated inflation cycles, it will fail first.
Inconsistent thickness across the same roll
Run your fingers along the edge of a fabric roll from one end to the other. You should feel uniform thickness. If you detect thin spots or raised ridges, the mill’s extrusion or coating process lacks control. For air beams, even a 0.1mm variation in coating thickness can create weak zones that balloon under pressure while adjacent areas remain rigid — an uneven stress distribution that guarantees premature failure.
Oily residue on hands after handling
Rub the fabric surface firmly with your palm for five seconds. If your hand comes away greasy or stained, plasticizer migration is already active — before production even starts. This is especially common on low-cost PVC-coated polyester where manufacturers cut costs by using high-migration plasticizers instead of polymer-grade alternatives.
How Kelyland Outdoors Builds Fabric Quality Into Inflatable Tents
A 300D shell can feel tough while the TPU/PVC-coated beam underneath is the real weak point — Kelyland’s factory network isolates both.
Most buyers fixate on the outer shell fabric when evaluating an inflatable tent. That’s understandable — it’s what the customer sees. But the structural integrity of an inflatable tent lives in the air beam fabric, and that’s where a sourcing partner like Kelyland Outdoors separates itself. The company’s network of 17 core strategic factories and over 200 manufacturing partners includes dedicated tent and air mattress facilities that specialize in coated fabrics for pressurized structures. When you spec a custom inflatable tent through Kelyland, the shell fabric (typically 150D to 300D polyester oxford) goes through one supply chain, while the beam fabric (PVC or TPU-coated) goes through another — each with its own quality control checkpoints.
Material Sourcing from Certified Mills
Kelyland sources shell and beam fabrics from mills that hold ISO 9001:2015 certification, which is a baseline requirement across its partner factories. For example, the camping tent and tarp factory in Ningbo (est. 2021, annual output of 800,000 units) and the glamping tent factory in Shaoxing (est. 2019, annual output of 300,000 units) both operate under CE and ISO 9001 standards. This means every roll of polyester oxford entering production has documented mill origin, denier verification, and coating thickness data. The air mattress factory in Xiangyang (est. 2020, annual output of 2.5 million units) adds ETL certification for built-in pump systems — relevant because many inflatable tents integrate electric inflation components.
The practical advantage for a brand manager is traceability. If a batch of shell fabric shows inconsistent hydrostatic head ratings or a beam develops plasticizer migration after six months of retail storage, Kelyland can trace it back to the specific mill lot and coating batch. That level of supply chain visibility is rare among generalist sourcing agents who simply broker orders between multiple unvetted workshops.
Fabric Dyeing and Coating Options for Private Label Brands
For private label projects, Kelyland offers Pantone-matched fabric dyeing across multiple printing methods — silk-screen, digital, thermal transfer — applied at the mill level before cutting and sewing. This matters because dye penetration affects coating adhesion: a poorly dyed base fabric can cause PU or silicone coatings to delaminate under UV exposure within two seasons. The company’s coating options include black coating (for superior UV block), silver coating, PU, silicone, and PVC — each selected based on whether it’s applied to shell panels or air beams.
결론
A tent’s fabric spec sheet is only half the story. The other half is how those numbers translate into real-world performance after a season of UV exposure and repeated inflation cycles. A 300D shell can feel tough in hand, but if the PVC-coated beam underneath suffers from plasticizer migration, the tent loses structural integrity within months.
-
- Tear strength matters more than denier for shell fabric durability.
- Request ISO 13937 tear test results before approving a production run.
- Fold a PVC beam sample for 24 hours to check for plasticizer migration.
- Specify separate coatings for shell and beam fabric in your build sheet.
If you’re sourcing your next inflatable tent line, use the spec checklist from this guide when reviewing supplier proposals. Ask for the ISO test reports and request a physical swatch to run the fold test yourself. A supplier that provides those documents without hesitation is one that understands how fabric failures affect your brand’s reputation on the retail floor.
자주 묻는 질문
How to get a quote for Inflatable Tent Fabric: Denier, Coating & Tear Strength?
정확한 답변은 제품 사양, 수량 및 주문 설정에 따라 달라집니다. 가장 안전한 접근 방식은 최종 요구 사항 시트가 확정된 후에만 상업적 조건을 확인하는 것입니다. 최종 선택은 실제 사용 사례와 성능 목표에 맞게 이루어져야 합니다.
먼저 샘플을 요청할 수 있을까요?
정확한 답변은 제품 사양, 수량 및 주문 설정에 따라 달라집니다. 가장 안전한 방법은 최종 요구 사항 시트가 확정된 후에만 상업 조건을 확인하는 것입니다. 샘플 가용성은 현재 재고 및 배송 계획에 따라 확인해야 합니다.

 English
 Español
 Deutsch
 Français
 Português do Brasil
 Русский
 العربية
 한국어
 日本語