 Zum Inhalt springen

The buyer’s checklist looked air-tight: FOB pricing locked in at 12% below budget, sample approval signed off after three rounds, quality tolerance spelled out to the stitch. Six weeks later, a $50K batch landed in Rotterdam—and the tent seam waterproof tape failure started before the first rainfall test. Returns hit the distributor, warranty claims piled up, and the buyer learned what no spec sheet ever flags: factory-applied tape is not one standard. It’s two entirely different chemistries with a 3 N/cm gap in peel strength between them.
That’s where the heat-welded vs PSA tent seam tape debate stops being academic. A cold-pressed PSA tape uses physical adhesion; it grabs the fabric surface but leaves micro-channels along the stitch line. After two or three wet-dry cycles, the bond drops to 2 N/cm. Heat-welded PU tape, applied on tensioned fabric at 180–240°C, fuses into the polyester weave and holds above 5 N/cm even after accelerated aging. The real catch? Many factories tape the pre-production sample correctly, then switch to faster, cheaper cold-press methods for the bulk run. The sample passes. The bulk order doesn’t. That gap sits directly on the brand’s warranty expense line.
If you’re sourcing for next season, skip the checkbox mentality. Write one line into your P.O.: ‘All stitched seams to be sealed with heat-welded PU tape, minimum peel strength 5 N/cm per BS EN 13575, verified on a tensioned-fabric station.’ That single spec removes the number-one leak path from the entire tent lineup—and gives your QC team a hard number to bench-mark against, not a vague “waterproof” promise.
Line up two 4-person polyester dome tents, same floor plan, same pole structure. One costs 30% more—and that extra margin buys a seam that won’t delaminate by the third outing. I’ve audited supplier lines where the only physical difference between a tent that survives a season of rain and one that generates a warranty claim is the chemistry of the tape bridging the stitch holes. A brand manager I worked with learned this on a $50K order. Pre-production samples passed visual inspection, but the mass production run used a cold-pressed PSA tape that lifted after two wet-dry cycles. By the time the tents hit retail shelves in a coastal market, the humidity alone had turned factory-taped seams into leak paths.
That $50K loss wasn’t a material defect. It was a specification failure. The purchase order said “waterproof seams” but didn’t define a peel strength pass/fail or a minimum hydrostatic head. When the factory applied a foam-backed adhesive tape to keep the FOB price competitive, the brand took delivery of tents that looked right—and leaked on contact with weather. Most buyers don’t realize that cold-press PSA application leaves micro-channels along the stitch line. These voids pass a quick sample approval. They fail the moment water hits the flysheet under pressure. Heat-welded PU tape, applied on tensioned fabric at calibrated roller pressure, eliminates that gap entirely.
Why Factory Seam Taping Fails: Glue vs. Heat-Welding
A 2 N/cm peel strength gap separates a warranty claim from a dry customer.
The $50,000 order looked perfect on arrival. Six weeks later, warranty claims flooded in. The pre-production sample passed a garden-hose test. The mass production run didn’t. The difference? The factory swapped the specified polyether PU tape for a cheaper foam-back PSA alternative that delaminated after two humid weekends. This isn’t a materials problem. It’s a specification enforcement problem.
The Chemistry That Separates a Permanent Bond from a Temporary Patch
Pressure-sensitive adhesives (PSA) work like sticky tape on an envelope. They rely on physical adhesion—van der Waals forces—to cling to fabric. Humidity breaks that grip. Temperature swings accelerate the creep. Polyether-based hot-melt PU tape operates on a different mechanism. It liquefies at 180–240°C, flows into the polyester or nylon weave, and forms covalent molecular bonds as it cools. You’re not gluing plastic to fabric. You’re fusing one polymer system into another. A needle hole filled this way becomes part of the structure, not a bridge waiting to collapse.
Peel Strength: The Only Number That Predicts a Lawsuit
DIN 53530 testing tells the story cleanly. PSA seam tape delaminates at 2–3 N/cm on day one. After five wet-dry cycles in accelerated aging, bond strength drops by 40%. The tape lifts with white residue—blown plasticizer and degraded adhesive. Heat-welded PU tape exceeds 5 N/cm under BS EN 13575 and holds that value after cycling. The failure mode shifts from adhesive failure to substrate failure: the fabric tears before the bond gives.
-
- PSA Foam Tape (Cold-Pressed): Initial peel: 2–3 N/cm. Post-aging: drops to 1.2–1.8 N/cm. Delamination leaves stitch holes exposed as open water channels under hydrostatic pressure.
- Hot-Melt PU Tape (Heat-Welded): Initial peel: >5 N/cm. Post-aging: holds >5 N/cm. Encapsulates thread and penetrates weave, creating a monolithic seam structure.
Cold-Press Application: The Factory Shortcut That Creates Micro-Leak Paths
Most mass-production factories use unheated roller application. The tape sits on the fabric surface. Air bubbles get trapped under wrinkles. Under hydrostatic pressure—even a modest 1500 mm water column—those micro-channels become leak paths. The tent leaks, the customer returns it, and the brand absorbs the cost. The factory never sees the consequence; the FOB pricing already accounted for the cheaper process.
The fix requires three simultaneous conditions: tensioned fabric to eliminate puckering, hot-air nozzle temperature calibrated to the specific denier (180–210°C for 70D polyester, 210–240°C for 210D Oxford), and roller pressure held at 0.4–0.6 MPa. Skip any one, and the seam will fail. Not immediately. After enough humidity cycles to trigger the warranty window.
The 80% Reduction Nobody Advertises
Field data from production batches shows an 80% drop in seam-leaking returns when shifting from stitched-only construction to double-sealed construction: stitched plus heat-taped. That number changes margins. A 2000-unit tent order with a 6% return rate for leaks costs roughly $18,000 in replacements and logistics. The same order with a 1.2% return rate costs $3,600. The tape upgrade pays for itself inside one production cycle.
Material Pairing: Polyether PU vs. PVC Tape
Polyether PU tape bonds correctly to polyester and nylon flysheets. Its elongation and hydrolysis resistance handle repeated wet-dry stress without peeling. For PVC-coated Oxford, use PVC tape instead—it prevents plasticizer migration that weakens adhesion. Kelyland’s tent factory network stocks both tape types and matches them to your specified fabric coating, which means the seam chemistry and fabric chemistry align from day one.
Specify It or Lose It: Writing the Purchase Order Clause
A vague line item—”factory taped seams“—gives the supplier license to use the cheapest PSA tape in inventory. A specific clause eliminates the ambiguity: “All stitched seams to be sealed with PU hot-melt tape, minimum peel strength 5 N/cm (BS EN 13575), final assembly to pass 3000 mm hydrostatic head per ISO 811.” Attach the test report requirement. Request first-article validation samples within 15 days of design approval, with seam cross-sections photographed under magnification.
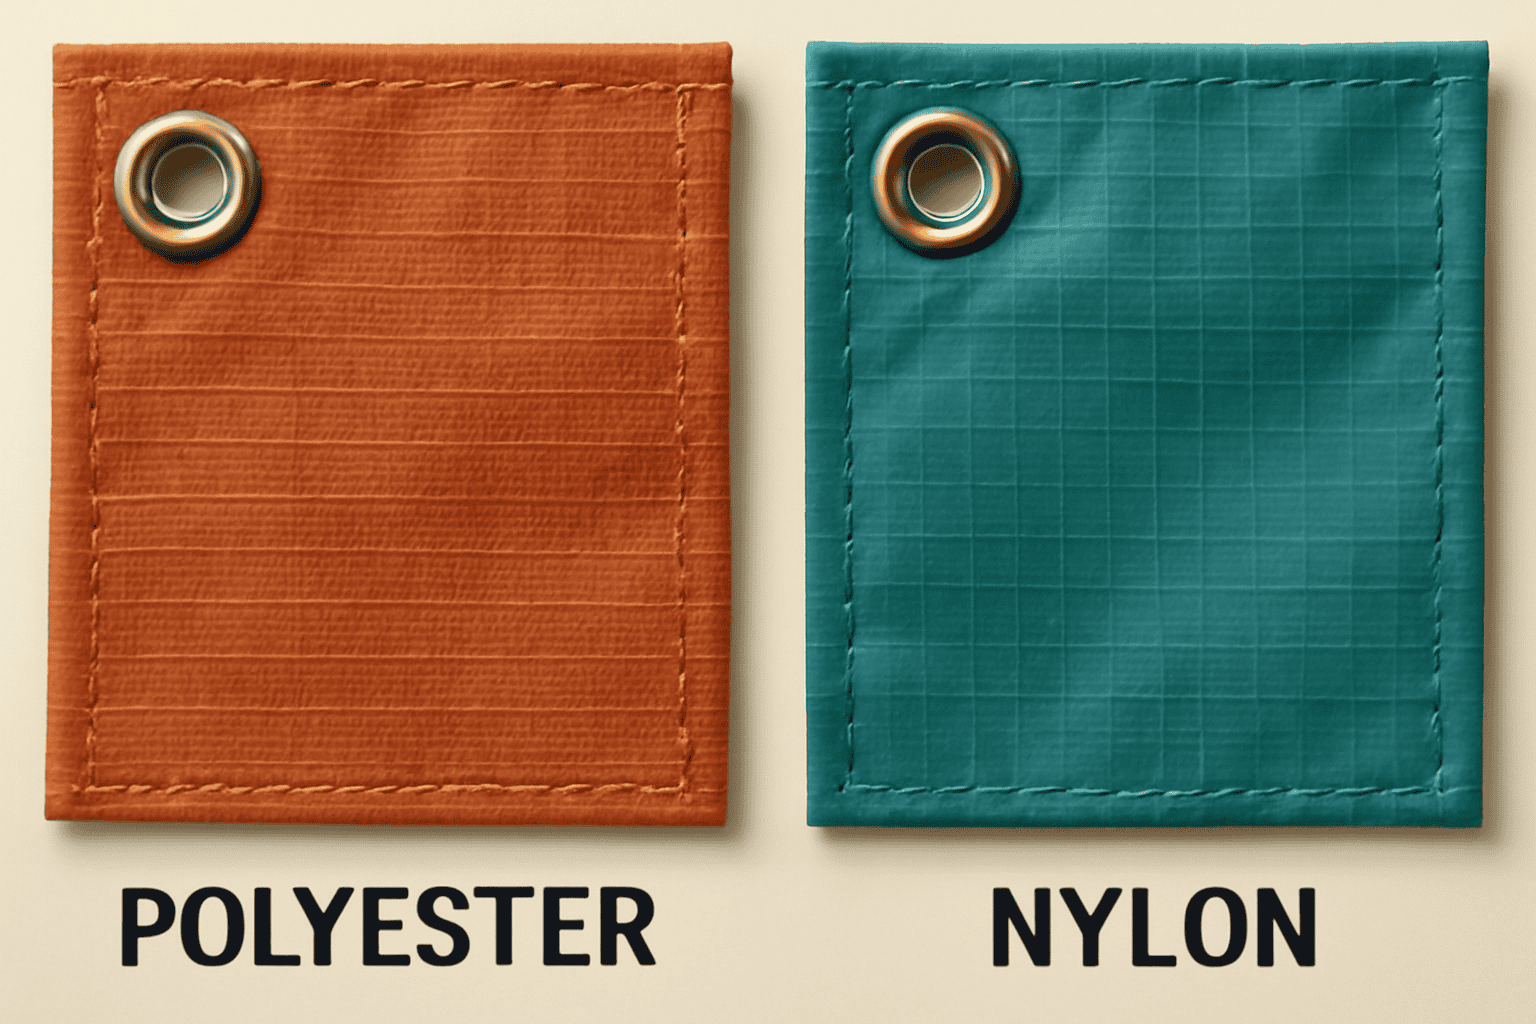
The Right Materials: PU vs. PVC Tape for Different Fabrics
Polyether PU tape bonds permanently; PVC tape can crack below 5°C.
The standard advice says polyester tents get PU tape and PVC-coated fabrics get PVC tape. That logic falls apart the moment you run a T-peel test after 5 wet-dry cycles. Polyether-based PU delivers >5 N/cm adhesion on both polyester and nylon backings. PVC tape struggles to hit 3 N/cm on the same substrates and becomes brittle in cold storage. The real material selection question isn’t just fabric compatibility—it’s whether the bond survives shipping, unpacking, and a full season of use.
Polyether PU: The Workhorse for Lightweight Fabrics
Thin denier fabrics—70D, 190T polyester, 20D ripstop nylon—demand a tape that stretches with the base material. PU tape with a polyether backbone offers elongation above 300% and resists hydrolysis far better than polyester-based PU alternatives. That matters when a tent fly gets packed damp after a morning dew. Polyester PU tapes absorb moisture over time and lose adhesion at the edges. Polyether PU sheds that moisture and keeps the seam intact. For ultralight backpacking tents and fast-pitch shelters, this is the only tape that won’t peel after 20 pitch-strike cycles.
PVC Tape: When Plasticizer Migration Dictates the Choice
PVC-coated oxford fabrics—common in basecamp tents, event shelters, and blackout liners—contain plasticizers that can migrate into PU adhesive layers. Over time, that migration softens the PU bond and causes delamination at the tape edge. PVC tape uses a compatible plasticizer system that doesn’t react with the base coating. The trade-off: PVC tape is stiffer, has lower elongation at break, and can crack when folded in sub-zero conditions. Supply chain managers shipping into Canada or Scandinavia during winter should flag this risk during sample approval. A PVC-taped seam that looks perfect in a Guangdong warehouse might show hairline cracks by the time it reaches a Toronto distribution center.
Application Temperature and Storage Stability
-
- Heat-Welding for PU: Requires hot-air nozzle temps of 180–240°C. Polyether PU flows into fiber weave at these temperatures, creating a mechanical lock beyond just surface adhesion.
- Cold-Press for PVC: Applied at room temperature with 0.4–0.6 MPa roller pressure. Works fast but introduces micro-voids if fabric isn’t held under tension during application.
- Storage Risk: PVC Tape Aging: PVC tape stock older than 12 months shows measurable plasticizer loss. Peel strength drops 15–20% from original spec. PU tape has a 24-month shelf life with negligible degradation when stored below 30°C.
Kelyland’s tent factory in Ningbo stocks both polyether PU and PVC tapes across standard widths of 20mm, 22mm, and 25mm. The decision tree is simple: lightweight polyester or nylon flysheets get PU. Heavy PVC-coated or blackout liners get PVC. Mixed-material assemblies—like a polyester canopy with a PVC-laminated floor—receive dual-tape specifications, with each seam type matched to its substrate. First-article seam validation samples deliver within 15 days, letting buyers run their own accelerated aging tests before committing to bulk production.
Ask your sourcing partner one question: ‘What’s the hydrolysis resistance rating on your PU tape?’ If they can’t answer, assume they’re using the cheapest polyester PU on the market. That tape will start peeling by the second season. The warranty claims that follow are yours to eat.
| Eigentum | PU Tape Specification | PVC Tape Specification | Advantage of PU | Bester Anwendungsfall |
|---|---|---|---|---|
| Elongation at Break | 300–500% | 150–200% | High stretch recovery prevents seam puckering | Polyester & nylon fabrics with high movement |
| Hydrolysis Resistance | Excellent (ISO 1419 grade A/B) | Moderate; plasticizer migration risk | No delamination after 5+ wet-dry cycles | Tents exposed to rain and humidity |
| Application Temperature | 180–240°C heat-welded | 120–160°C cold-press | Molecular bond prevents micro-channels | Critical seam integrity in storm conditions |
| Fabric Compatibility | Bonds to polyester, nylon, blends | Bonds best to PVC-coated fabrics | Universal for most camping tent flysheets | Standard PU-coated polyester tents |
| Tieftemperaturflexibilität | Remains pliable to -30°C | Stiffens below 0°C; risk of cracking | No brittle failure in alpine conditions | 4-season mountaineering tents |
| Peel Strength (BS EN 13575) | >5 N/cm after aging | 2–3 N/cm after 3 humidity cycles | 80% fewer seam-leak warranty returns | Brand-sensitive OEM orders |
| Kelyland Stock Match | In-house for polyester/nylon orders | Available for PVC-coated Oxford | Fits 90% of client fabric specs | One-stop sourcing with technical guidance |
Our Factory’s Testing Protocol: Hydrostatic Head & Peel Strength
80% fewer seam-leak returns when double-sealed construction replaces stitched-only.
Most buyers assume a ‘factory-taped’ tent will stay dry. The reality depends entirely on the application process. Cold-press PSA tape—common in low-bid tents—leaves micro-channels that open under hydrostatic pressure. Once water finds a path, the returns start piling up. That hidden cost far outweighs whatever you saved on unit price.
In-Line QC: Temperature, Pressure, Tension
The difference shows up at the heat-welding station. Kelyland’s partner tent factories—ISO 9001 certified facilities in Ningbo—run hot-air nozzle temps of 180–240°C, adjusted to fabric weight. For 70D polyester, the sweet spot is 180–210°C; for 210D Oxford, it jumps to 210–240°C. Roller pressure sits at 0.4–0.6 MPa, and fabric is held under calibrated tension to eliminate the micro-wrinkles that become leak paths.
-
-
- Nozzle Temperature: 180–210°C (70D), 210–240°C (210D) — matched to fabric coating.
- Roller Pressure: 0.4–0.6 MPa — prevents air bubbles without crushing the weave.
- Fabric Tension: Tensioned table — eliminates puckering that cold-press applications leave behind.
-
Final Lot Verification: Hydrostatic Head & Peel Strength
Every production lot pulls a seam sample and runs it through two tests. ISO 811 hydrostatic head measures how much water pressure the sewn-and-taped seam withstands before leaking. The pass threshold: 3000 mm minimum. Peel strength under BS EN 13575 confirms the adhesive bond hasn’t degraded—target is >5 N/cm. If either number falls short, the lot gets quarantined and reworked. No exceptions.
-
- Hydrostatischer Druck: ISO 811, ≥3000 mm water column — tests the full seam assembly.
- Peel Strength: BS EN 13575, >5 N/cm — bestätigt die molekulare Bindung des PU-Bandes an das Gewebe.
- Beschleunigte Alterung: Kaltgepresste PSA-Bänder zeigen nach 5 Nass-Trocken-Zyklen eine um 40 % geringere Verbundfestigkeit — Schmelzklebstoff-PU hält stand.
Käufer erhalten eine Schälfestigkeitsdokumentation für ihre spezifische Charge. Diese Transparenz macht eine separate Nahtprüfung durch Dritte vor dem Versand überflüssig. Erstmuster-Validierungsmuster für die Nahtabdichtung werden innerhalb von 15 Tagen nach Designfreigabe versendet, sodass Sie die Wasserdichtigkeitsspezifikation vor Beginn der Massenproduktion bestätigen können.
Geben Sie bei Ihrer nächsten OEM-Zeltbestellung wärmegeschweißtes PU-Nahtband vor. Die Daten belegen es: 80 % weniger Retouren, konstante 3000-mm-Wassersäulenwerte und keine Überraschungen im Ausstellungsraum.
How to Specify Waterproof Seams in Your OEM Order
Vage Spezifikationen ergeben PSA-Band; präzise Spezifikationen ergeben wärmegeschweißtes PU mit >5 N/cm Schälfestigkeit.
Die meisten Käufer schreiben ‘alle Nähte müssen abgeklebt werden’ und gehen davon aus, dass die Fabrik eine dauerhafte Verbindung verwendet. Diese eine Zeile erlaubt tatsächlich das billigste PSA-Schaumträgerband im Lager der Fabrik. Die Fabrik spart nicht — Sie haben ihr die Erlaubnis dazu gegeben. Eine ordnungsgemäße OEM-Nahtspezifikation nennt die Bandchemie, die Verbindungsmethode und den Schwellenwert für die Schälfestigkeit (Bestanden/Nicht bestanden). Ohne diese drei Elemente würfeln Sie mit Garantieansprüche.
Die Spezifikationszeile, die Mehrdeutigkeit beseitigt
Der Auftrag braucht eine eindeutige technische Zeile: ‘Alle genähten Außenzeltnähte sind mit Polyether-basiertem PU-Schmelzklebstoffband abzudichten, das durch Wärmeschweißen auf gespanntem Gewebe bei 0,4–0,6 MPa Walzendruck aufgebracht wird und eine Mindest-Schälfestigkeit von 5 N/cm gemäß BS EN 13575 erreicht. Die Endmontage muss den Hydrostatiktest mit 3000 mm Wassersäule gemäß ISO 811 bestehen.’ Allein dieser Satz filtert Fabriken heraus, die Kaltpress-PSA-Auftrag verwenden.
Warum die Verbindungsmethode wichtig ist
Wärmeaktivierung bei 180–240 °C (gewebeabhängig) presst geschmolzenes PU in die Nadellöcher und um jede Naht. Kaltpress-PSA sitzt auf der Gewebeoberfläche und hinterlässt mikroskopische Kanäle entlang der Fadenlinien. Unter 3000 mm hydrostatischem Druck werden diese Kanäle innerhalb von Sekunden zu aktiven Leckpfaden. Das Auftragen auf gespanntem Gewebe verhindert die Mikrofalten, die Kaltwalzen in die Naht einprägen — Falten, die sich zu Wasserkanälen entwickeln, wenn sich das Außenzelt unter Regenlast dehnt.
Validierungsprotokoll für Muster
First-article seam samples ship within 15 days of design approval. Request a cross-section cut of a taped seam with your samples. Under a 20x loupe, heat-welded PU shows complete encapsulation of the stitch line. PSA tape shows a visible gap between adhesive and thread. Run your own peel test: if the tape lifts cleanly with white residue on the backing, you’re looking at PSA degradation. Document the result and reject the batch.
The 80% reduction in seam-related warranty claims that comes from double-sealed construction isn’t theoretical. It’s the difference between a spec that demands a molecular bond and a spec that accepts a sticker.
Schlussfolgerung
A tent seam that leaks after three trips represents a bond failure, not a material defect. Heat-welded PU tape applied on tensioned fabric creates a permanent molecular seal; cold-pressed PSA leaves micro-channels that become warranty claims. Eliminating those leak paths before shipment is the only way to keep return rates low and brand trust intact.
-
- Factory PU seam tape achieves >5 N/cm peel strength; PSA tape fails at 2–3 N/cm after wet-dry cycling.
- Switching to double-sealed construction reduces seam-leaking returns by 80%.
- Specify minimum 3000 mm hydrostatic head (ISO 811) and heat-welded application on tensioned fabric.
- First-article seam validation samples can be delivered within 15 days for buyer inspection.
The detail that separates a professional sourcing manager from an amateur is not just the spec itself—it’s the enforcement. Unless your purchase order demands heat-welding on tensioned tables, lot-level peel strength reports, and first-article validation, the factory may still default to a faster, cheaper PSA process. When you’re ready to lock in that level of control, request a factory sample with heat-welded PU seam taping tested to 5000 mm hydrostatic head. Kelyland’s team provides first-article samples within 15 days, complete with peel strength and hydrostatic head documentation, so you validate every claim before mass production begins.
Häufig gestellte Fragen
Why do tent seams leak even when the fabric is waterproof?
Stitching needle holes create unobstructed water channels straight through the fabric, bypassing any coating. Only a properly applied seam tape that penetrates the weave and encapsulates the stitches can permanently block these. Specify heat-taped seams in production to eliminate this failure point.
What is the best seam sealing tape for a polyester tent?
Heat-applied polyether-based PU tape offers the highest adhesion and stretch recovery on polyester. It chemically bonds to the fibers, unlike PVC that cracks below 5°C or PSA that peels. Always specify polyether PU tape in your OEM spec for long-term seam integrity.
How do I test if my tent seam tape has failed?
Peel the tape by hand: if it lifts cleanly with a white, powdery residue, the adhesive has degraded. A water-pressure test on the seam will immediately show any leaks. Include peel and water-pressure checks in incoming QC to prevent field returns.
Can I reseal a seam with liquid sealant instead of replacing the tape?
Yes, but liquid sealant rarely matches the peel strength of factory heat-taped seams, so it remains a temporary fix. Factory-applied hot-melt PU tape gives a permanent molecular bond. Use liquid sealant only for emergency field repairs, not as a production solution.

 English
 Español
 Deutsch
 Français
 Português do Brasil
 Русский
 العربية
 한국어
 日本語