 跳到内容

Un taux de rejet de 37 % lors d’un contrôle pré-expédition, c’est le genre de chiffre qui Figés les responsables de la supply chain. Voici le résultat du contrôle qualité d’une tente gonflable pour douze personnes destinée à une chaîne de vente au détail — une commande de 500 pièces dont le fournisseur avait déjà validé l’aspect visuel avec son propre service QC interne, manquant systématiquement des défauts de soudure cachés qui auraient provoqué des retours produits trois mois plus tard.
La cause racine n’était ni malveillante ni même exceptionnelle. La température d’une machine de soudure a dérivé après un réglage en cours de production, et l’équipe a continué à produire sans vérifier la rétention d’air pendant le poste. L’échantillon fait main que l’acheteur avait validé avait été soudé sur une autre machine, à vitesse réduite, et avait passé tous les contrôles esthétiques. La production en série a utilisé un processus plus chaud et plus rapide, créant une délaminage invisible autour des connexions poutre-plancher et une séparation à la base des clapets au niveau des joints de soudure — des défauts qu’aucune inspection visuelle AQL 2.5 ne pourra jamais détecter, car la plupart des fuites sont invisibles jusqu’à ce que la tente soit gonflée et laissée sans surveillance pendant plusieurs heures.
C’est pourquoi le test de rétention sous pression doit figurer comme ligne budgétaire distincte dans le contrat, et non comme une simple pensée tardive glissée dans la checklist QC. Un protocole d’inspection pré-expédition standard pour les tentes gonflables, sans test de rétention d’air, est fonctionnellement inutile pour cette catégorie de produits. La référence que vous devez inscrire pour votre prochain appel fournisseur : toute usine produisant des structures gonflables doit être capable de démontrer une chute de pression maximale inférieure à 10 % sur douze heures pour chaque unité, avant emballage.
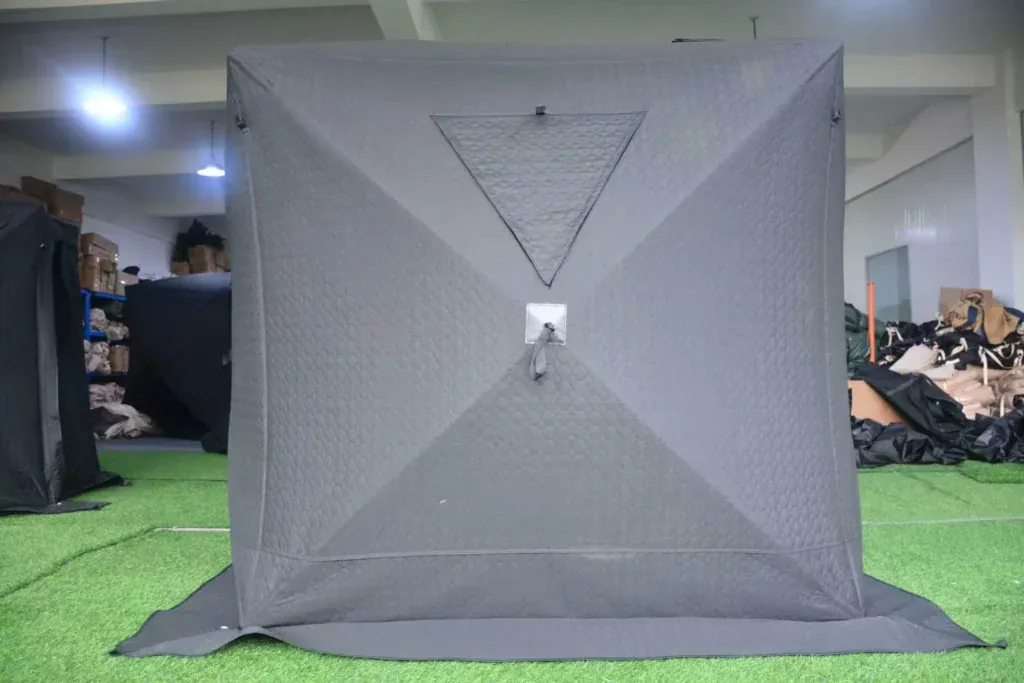
Ce qu’a révélé le contrôle pré-expédition
Un simple contrôle visuel AQL 2.5 passe à côté de toutes les fuites d’air critiques.
L’inspecteur tierce partie de l’acheteur est arrivé à l’usine au jour 38 d’un délai de 45 jours. Le fournisseur avait déjà émis son propre rapport QC, affichant un taux de réussite de 98 % aux contrôles visuels. Les coutures étaient droites, les fermetures éclair coulissaient bien, l’emplacement du logo semblait correct. L’inspecteur a tiré 80 unités au hasard dans le lot de 500 pièces, selon un échantillonnage aléatoire de niveau AQL II.
37 % ont échoué au test de chute de pression
L’inspecteur a gonflé chaque tente échantillon à la pression de service spécifiée, a hermétiquement fermé tous les clapets, et les a laissées reposer pendant 12 heures. Dès la sixième heure, 30 des 80 tentes avaient perdu plus de 15 % de leur pression interne. Il ne s’agit pas d’une fuite lente due à un trou d’épingle, mais d’une défaillance structurelle du système de rétention d’air. Une inspection AQL 2.5 standard aurait validé ces unités, car les fuites restent invisibles tant que la tente ne conserve pas la pression sur la durée.
Valve base separation at weld joints
Closer examination showed the problem was concentrated at valve bases where the TPU-coated fabric meets the welded flange. In 12 cases, the weld bead had separated from the base material by less than half a millimeter — enough to bleed air overnight but invisible to a visual inspector running a tape measure down stitch lines. The root cause traced back to one welding station where temperature drifted after a mid-run adjustment.
Delamination around beam-to-floor connections
Eight tents showed delamination along the beam-to-floor weld seams where main air beams attach to the floor panel. This area undergoes repeated stress during inflation and deflation cycles in field use. The delamination pattern suggested inconsistent heat pressure during RF welding — likely because production used a different welding process than what created the handmade sample approved three weeks earlier.
Logo placement and color inconsistencies
Où le processus a failli
The sample looked perfect.
The buyer approved the pre-production sample based on how it looked. Seams were straight, zippers ran smooth, the fabric color matched the Pantone code. No one inflated it and left it standing for 12 hours to see if the air stayed inside.
No inline inspection during welding
The factory ran three HF welding machines across two shifts. On day four of production, machine #2’s temperature controller drifted 8°C above the set point after a mid-run adjustment by the line operator. That shift produced 87 tents with partial delamination at the beam-to-floor joints. The inline inspector assigned to that line was checking stitch quality on the fabric panels — not weld integrity.
QC checklist skipped pressure testing
The supplier’s QC checklist had 23 inspection points: zipper function, thread tension, logo alignment, fabric color, seam allowance. Zero items related to air retention. This is common in factories that treat inflatable tents like conventional tents with an added tube pocket. A standard AQL 2.5 visual inspection will not catch air retention defects because most leaks are invisible until the tent is inflated and left untouched for hours.
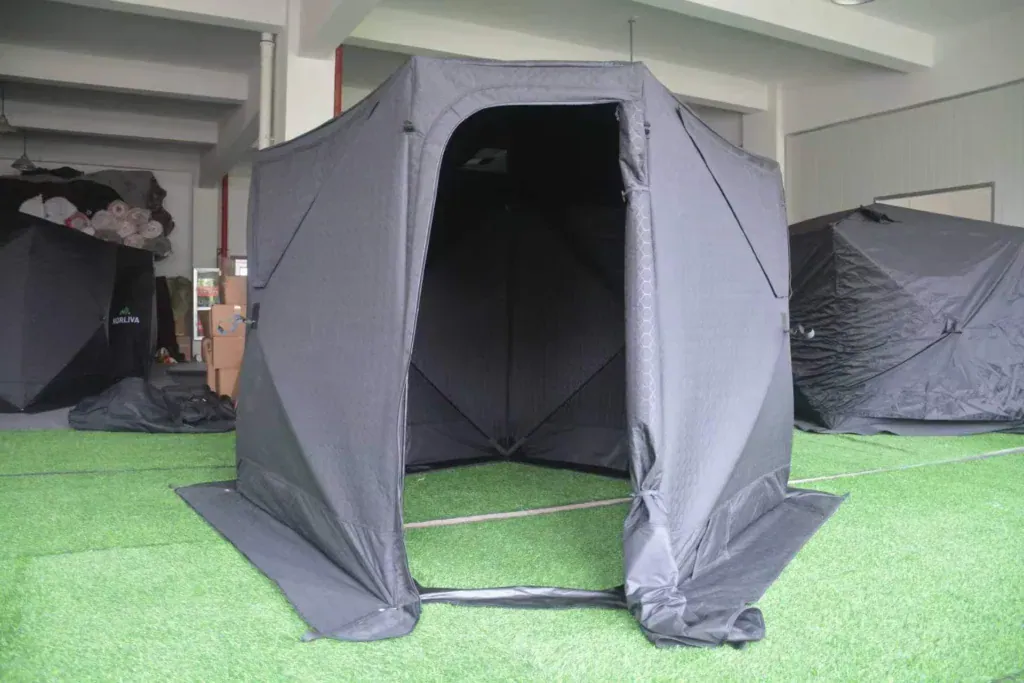
Rework decisions by production, not quality
When the pre-shipment inspector flagged the pressure drop failures, the factory’s production manager authorized a patch-and-reinflate fix on all failed units without consulting quality control or informing the buyer first. The patches held for an hour but failed overnight in 14 of 37 reworked tents. By that point, the container loading slot was already booked.
Comment une checklist QC structurée aurait permis de le détecter
A standard AQL 2.5 visual inspection misses air retention defects entirely.
The first fix is a pre-production meeting where the buyer and factory agree on pressure drop limits in writing. For a twelve-person glamping tent with a target operating pressure of 8 psi, the acceptable loss over 12 hours should be defined before the first meter of fabric is cut. Without this number, there is no pass/fail criteria.
First Article Inspection After the First 50 Pieces
After the first 50 units come off the line, stop production and test them. This catches drift early. In this case, one welding machine’s temperature drifted after a mid-run adjustment — that would have been visible in the first article batch if anyone had inflated those tents and measured pressure loss.
Random Sampling at 25%, 50%, and 75% of Production
Three sampling gates during production build a trend line. If failure rates climb at the 50% mark, you can halt rework before another 250 units are welded. The supplier’s QC team needs to run an air retention test on a fixed sample size at each gate, not just a visual check of seam appearance.
Final Pre-Shipment Inspection With Clear Pass/Fail Criteria
The final inspection must include an air retention test as a separate contract line item — not buried inside an AQL visual checklist. The standard used by Kelyland Outdoors’ partner factories, which operate under ISO 9001:2015 protocols, includes inline welding checks and documented pressure testing before packing. That level of process control turns a subjective review into a measurable pass or fail.
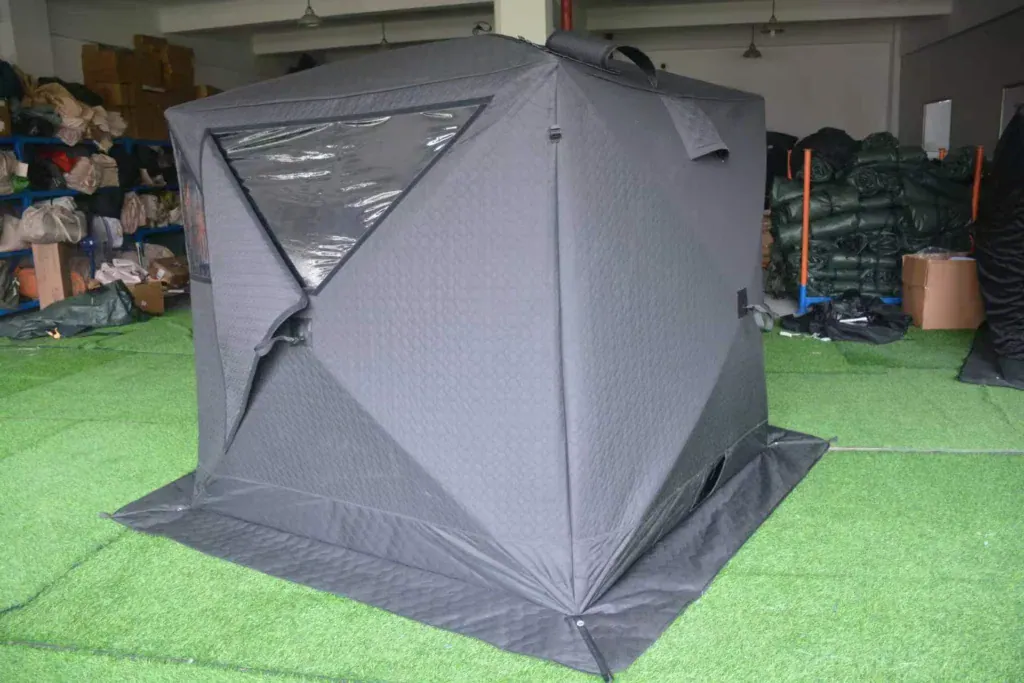
Ce qu’a fait l’acheteur par la suite
The buyer turned a $50K near-miss into a permanent process upgrade.
The supply chain manager didn’t cancel the order. That would have meant losing the season entirely, with a retail launch already locked in for April. Instead, he negotiated rework terms directly with the factory owner. Every tent that failed the pressure test — 185 units out of 500 — was pulled from the shipping batch and sent back to the welding station. The factory covered all material costs and labor for re-welding every valve base and beam-to-floor joint. The buyer agreed to split the expedited shipping fee to keep the delivery window intact.
Negotiated Rework, Not Full Rejection
Full rejection would have triggered a six-month production delay at a different supplier. Rework cost the factory roughly $12 per unit in additional labor and materials, versus an estimated $85 per unit in lost margin if the order was scrapped. The math worked for both sides. But the buyer made one thing clear: this was a one-time concession. Future orders would require documented proof of air retention testing before any shipment left the factory floor.
Implemented a Mandatory Air Retention Test on All Future Orders
The old contract specified visual inspection only — standard AQL 2.5 sampling on stitching, zippers, and fabric defects. That caught nothing on air retention because most leaks are invisible until the tent holds pressure for hours. The new contract added a separate line item: 100% inflation testing on every unit, with a maximum allowable pressure drop of 10% over 12 hours at room temperature. Any unit exceeding that threshold gets flagged for weld inspection before packing.
Added a Line-Item for Weld Inspections in the Production Contract
The revised contract now specifies inline weld checks at three points: after the first 50 units (first article inspection), at 50% of production volume, and again during pre-shipment inspection. Each check includes both visual examination of weld bead consistency and a short-duration pressure hold test on randomly selected units from that batch. This mirrors how partner factories in Kelyland Outdoors’ network handle inflatable tent production — with inline welding checks and documented pass/fail criteria before bulk assembly continues.
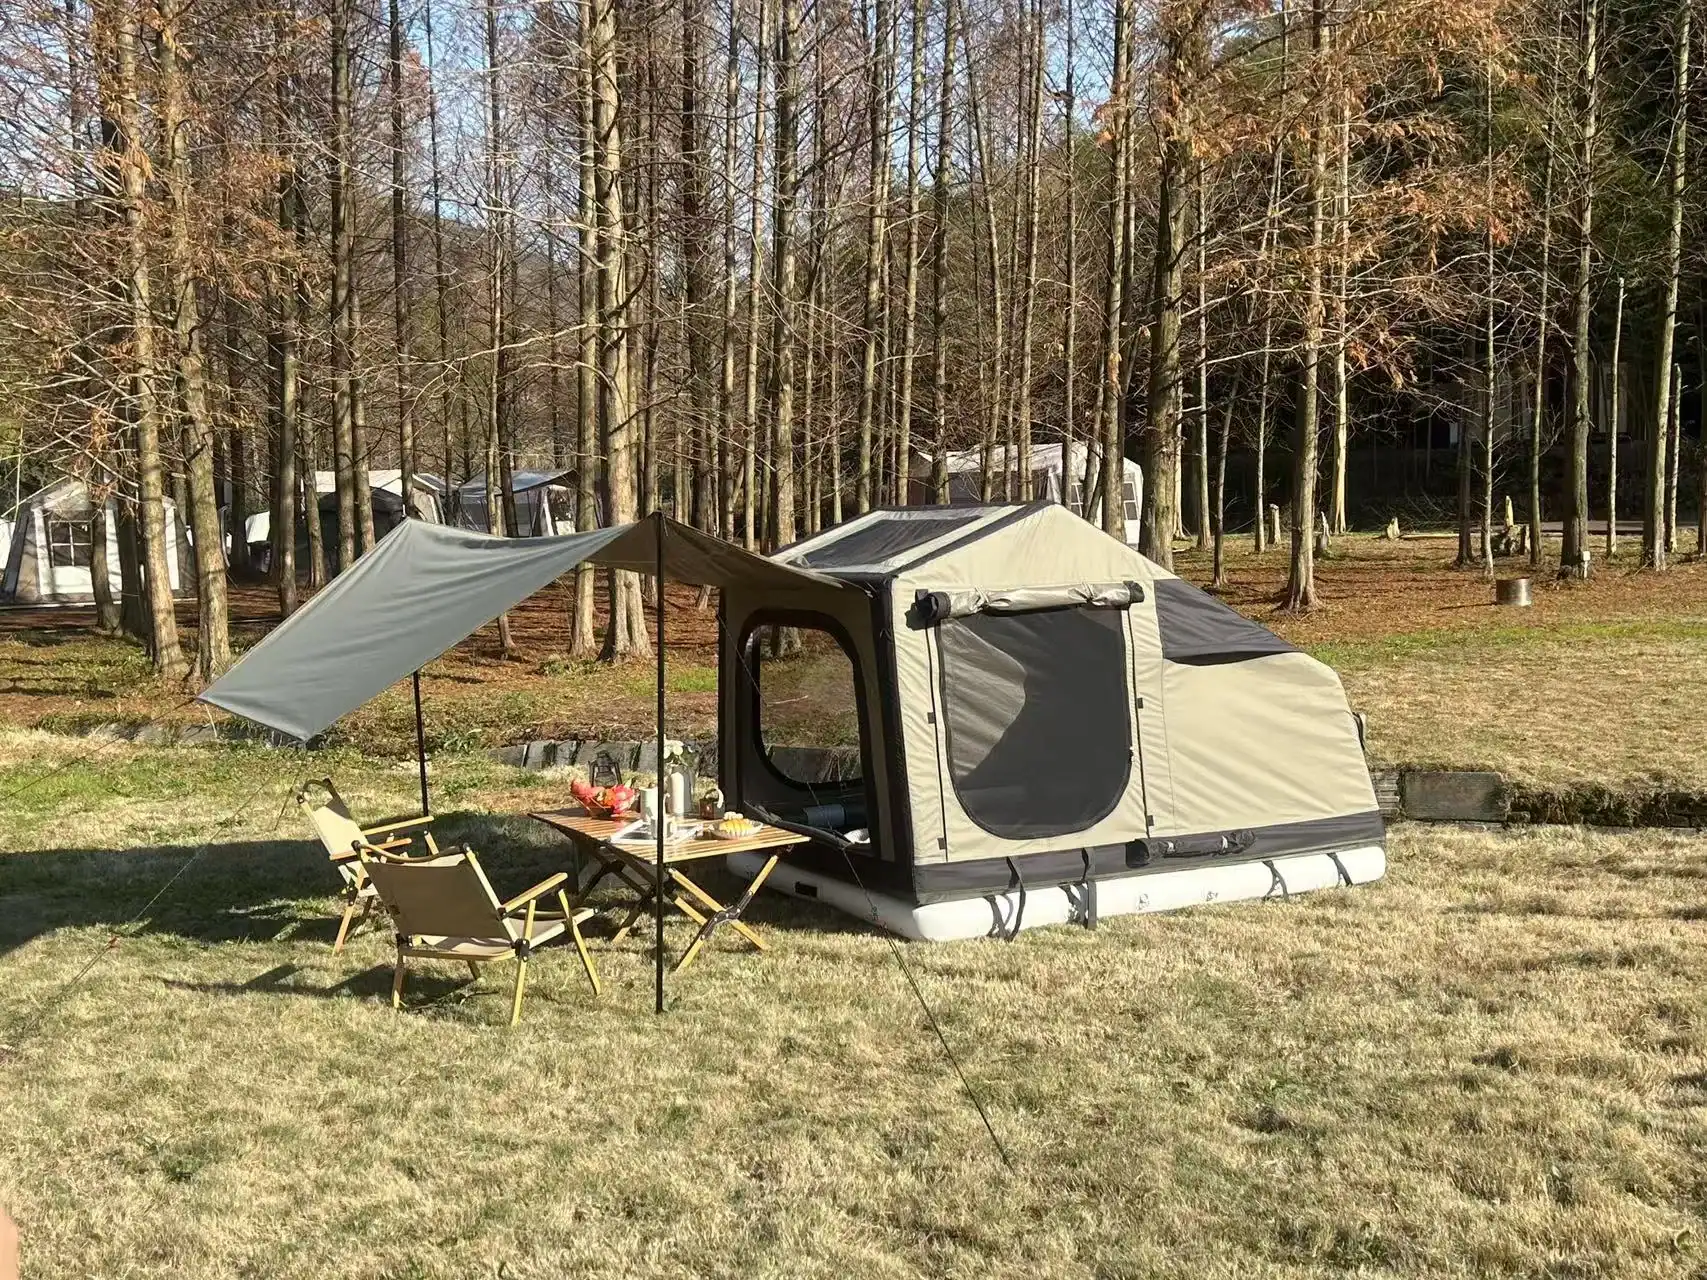
Comment Kelyland Outdoors prévient ces défaillances
Three QC steps that directly address the welding drift and invisible leak failures from the 500-piece case study.
The 500-piece order failure traced back to a single root cause: a welding machine whose temperature drifted after a mid-run adjustment. The factory’s QC team was checking visual appearance only, so no one caught it until the buyer’s pre-shipment inspection flagged 37% of units for pressure loss. That scenario repeats across inflatable tent sourcing because most suppliers treat air retention as a design assumption, not a production variable.
100% Inflation Testing Before Packing
A standard AQL 2.5 visual inspection will not catch air retention defects. Most leaks are invisible until the tent is inflated and left untouched for hours. At Kelyland Outdoors, every inflatable tent unit — whether from the Xiangyang air mattress factory (2.5 million units annual capacity) or the Ningbo tent factory — undergoes a full inflation hold test before packing. Each unit is inflated to rated pressure, sealed, and monitored for at least 30 minutes. Units that lose more than 5% pressure are flagged for weld inspection and rework.
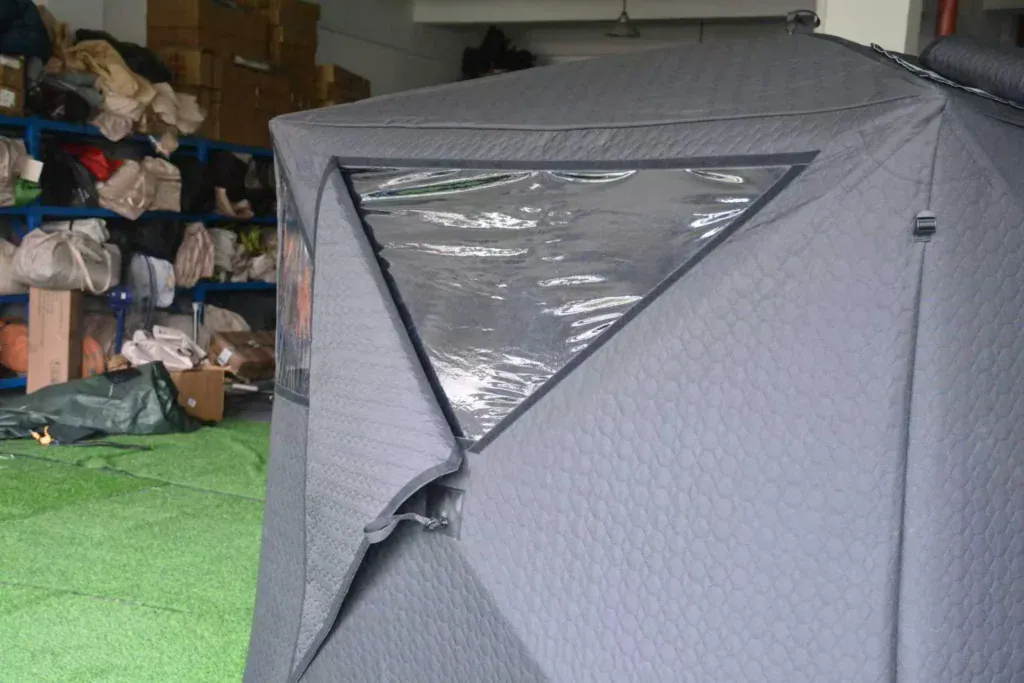
Inline Welding Checks at Strategic Factories
The case study’s welding drift happened because inspectors only checked finished tents. By then, all 500 units had passed through the same drifting machine. The fix is inline checks during production, not after. Kelyland’s partner factories — including ISO 9001:2015 certified facilities in Zhejiang and Hubei — run weld temperature verification every 50 joints during mass production runs. If a machine drifts by more than ±5°C from the approved spec, production stops until recalibration is confirmed.
Clear QC Deliverables for Every Order
The supplier in the case study had no written pressure drop limit in their QC checklist. The buyer hadn’t specified one either. That gap is common when sample approval focuses on aesthetics alone — handmade samples look great but hide process inconsistencies from mass production tooling. Kelyland Outdoors includes three mandatory QC deliverables in every inflatable tent contract: a signed first article inspection report after the first 50 pieces, an inline weld temperature log from each production shift, and a final air retention test result with pass/fail thresholds agreed during pre-production.
Conclusion
That $50K order was salvaged through rework, but the timeline blew past the retail launch window. A standard AQL 2.5 visual inspection missed every air retention defect because those leaks only show up after hours of inflation. The fix isn’t a better inspector — it’s a contract line item for a 12-hour pressure-hold test.
-
- 37% of units failed a 12-hour pressure drop test in this case.
- Visual-only sample approval misses weld defects from mass production.
- Pressure-hold testing must be a separate contract line item.
- Inline welding checks catch temperature drift before it affects the batch.
Before you approve your next inflatable tent production run, ask your supplier three yes/no questions from the checklist above — starting with whether their QC protocol includes an air retention test on every unit, not just a visual pass. If they hesitate on the pressure-hold spec, you already know where this story heads. Review how Kelyland Outdoors builds that test into every order by browsing our inflatable tent and air mattress production standards.
Questions fréquemment posées
How to get a quote for Inflatable Tent QC Failure: 500-Piece Order Case Study?
La réponse exacte dépend de la spécification du produit, de la quantité et de la configuration de la commande. L'approche la plus sûre est de confirmer les conditions commerciales uniquement après le verrouillage de la fiche d'exigences finale. Les conditions finales doivent être confirmées en fonction de la spécification exacte du produit et des conditions de commande.
Puis-je d'abord demander des échantillons ?
La réponse exacte dépend de la spécification du produit, de la quantité et de la configuration de la commande. L'approche la plus sûre est de confirmer les conditions commerciales uniquement après que la fiche d'exigences finale soit verrouillée. La disponibilité des échantillons doit être confirmée en fonction du stock actuel et du plan d'expédition.

 English
 Español
 Deutsch
 Français
 Português do Brasil
 Русский
 العربية
 한국어
 日本語